LOW PHOSPHORUS / ELECTROLESS NICKEL
Low-phosphorus electroless nickel
Low-temperature / ultra-low-P and low-P: two process groups, selected as needed.
Low-temperature low-P, ultra-low-P and extremely-low-P continuous types are grouped together for easy comparison around lower bath temperature or lower phosphorus content; the 1%–3% low-P option is shown as a separate group. Operating temperature and coating characteristics are listed for each product.
The following are product data and historical reference data, not guarantees for any workpiece; formal specifications are subject to engineer confirmation and the quotation.
Two process groups, each product's parameters compared separately
On mobile, swipe left and right; the first column keeps the comparison items.
| Selection parameter | Low-temperature low-P | Ultra-low-P | Extremely-low-P continuous type | Low-P |
|---|---|---|---|---|
| Group | Low-temp / ultra-low-P options | Low-P option | ||
| Coating phosphorus content | 2±1% | 0.5%–1% | Below 1% (continuous operation) | 1%–3% |
| Operating temperature | 75℃ | 88–94℃ | 83–87℃ | 85–90℃ |
| pH | 6.80±0.10 | 6.00±0.10 | 6.00±0.10 | 6.40±0.10 |
| Nickel plating rate | 14±2 μm/h (fresh bath, 75℃) | 10±2 μm/h (fresh bath, 90℃) | 11±2 μm/h (at make-up, 85℃) | 17±2 μm/h (fresh bath, 87℃) |
| Coating hardness | HV 600 or above achievable (without heat treatment) | HV 700 (after electroless plating) | — | HV 650 (after electroless plating) |
Plating rates come from fresh-bath conditions at different temperatures for each version and do not represent a performance ranking under the same conditions. First choose the required process, then check temperature, coating composition and heat treatment state; these values cannot be used directly as acceptance criteria for all workpieces.
01 / Selecting for lower bath temperature or lower phosphorus content
Low-temp / ultra-low-P options
This group contains three independent processes. The low-temperature low-P type operates at 75℃; the ultra-low-P and extremely-low-P continuous types operate at 88–94℃ and 83–87℃ respectively, chosen according to coating composition and production line conditions.
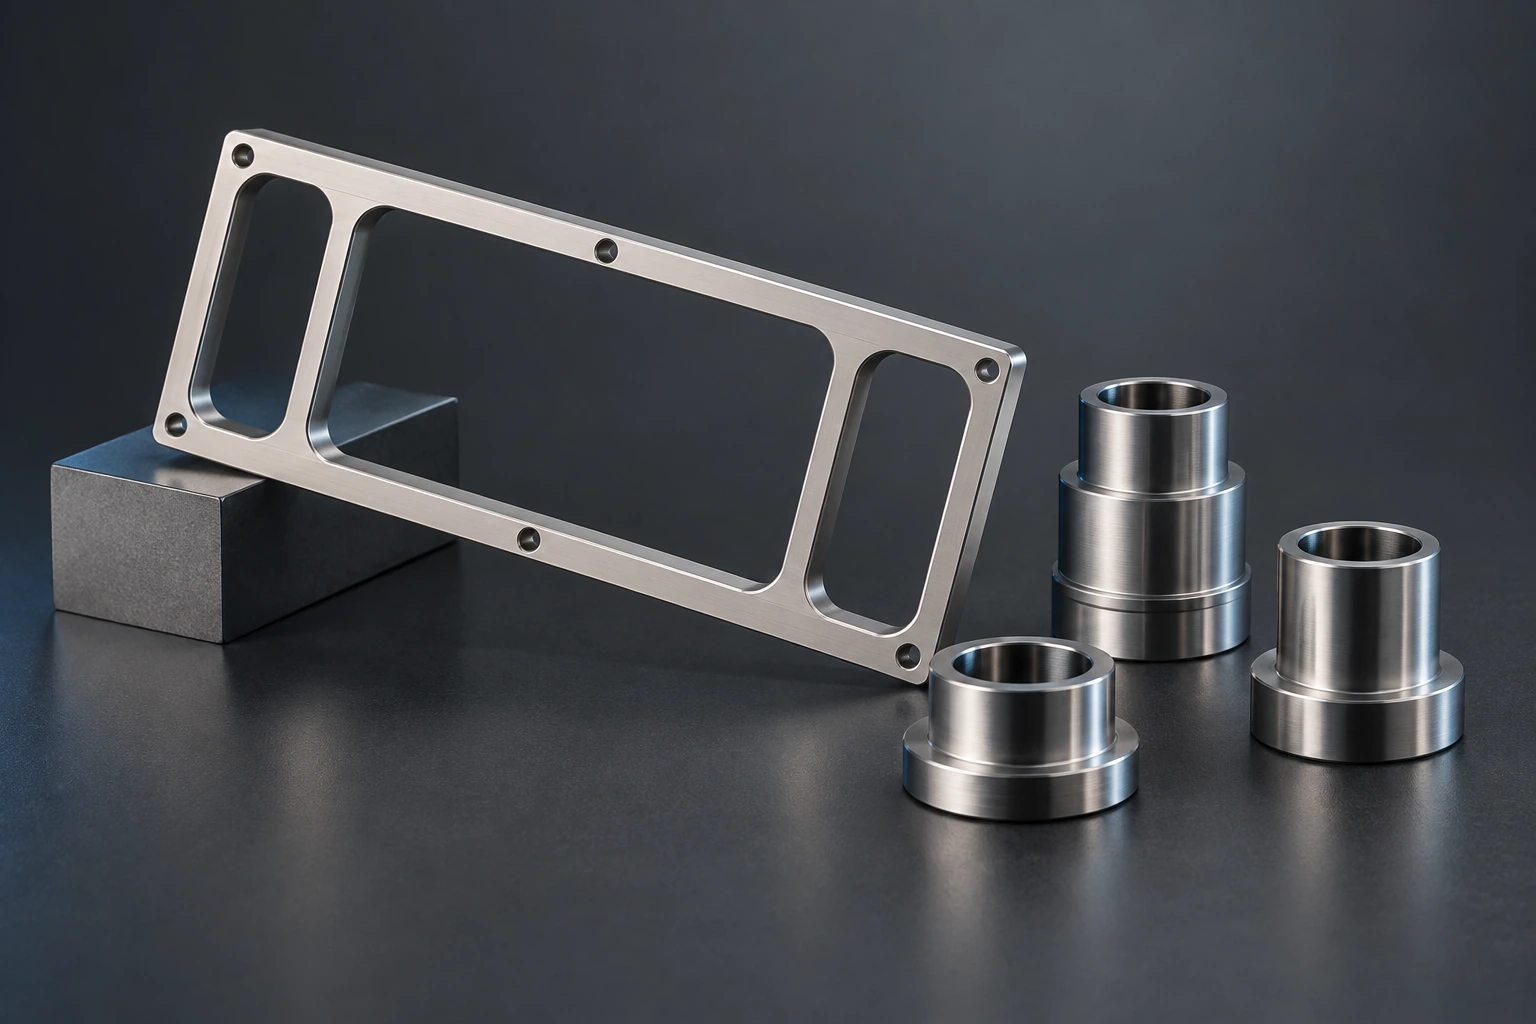
01 / 75℃ low-temperature process, combining low P with wear resistance.
Low-temperature low-P
Lead-free electroless nickel bath
This is a lead-free low-temperature low-P electroless nickel bath that can continuously perform Ni-P electroless plating at 75℃, with a coating phosphorus content of 2±1%. Coating hardness without heat treatment can reach HV 600 or above, along with good wear resistance, low volume resistivity and magnetic coating characteristics. Suited to process selection focused on lower operating temperature and low-P coating performance, and compatible with automatic analysis and replenishment for bath management.
Lower operating temperature
The manual specifies an operating temperature of 75℃, offering an option for processes that care about lower bath temperature.
As-plated hardness & wear resistance
Coating hardness without heat treatment can reach HV 600 or above, with good wear resistance.
Suited to continuous management
Supports automatic analysis and replenishment, helping maintain bath conditions and stable quality.
Process parameters
- Coating phosphorus content
- 2±1%Instructions p.3
- Operating temperature
- 75℃Manual operating conditions
- pH
- 6.80±0.10
- Nickel plating rate
- 14±2 μm/hFresh bath, 75℃
- Nickel sulfate concentration
- 24.0±2 g/Las NiSO₄·6H₂O
- Bath load ratio V/A
- 8–20bath volume mL / workpiece surface area cm²
- Coating hardness
- HV 600 or above achievablewithout heat treatment
Application directions & confirmation conditions
Selection based on typical uses of low-P coatings combined with a lower bath temperature.
Molds & forming tooling
Molds · plungers · precision tooling
Workpieces that need as-plated hardness and surface wear resistance, and where production at a lower bath temperature is desired, can evaluate this low-temperature process.
Suitability of low-temperature conditions must be confirmed with substrate and pretreatment.
Valves & precision transmission
Valve parts · gearbox components
For wear resistance needs on moving mating surfaces, trial plating selection can combine industry uses of low-P coatings with this product's 75℃ process conditions.
Coating thickness and fit tolerances must be checked at the same time.
Electronic connectors
Connectors · electronic terminals
Connectors requiring low volume resistivity and coating hardness can be included in application evaluation; assembly reliability should be tested with the connection structure.
Verify around contact resistance, connection method and service environment.
The instructions state: without heat treatment, coating hardness can reach HV 600 or above. The continuous test chart on p.9 of the technical data shows about HV 650, a test reference value, not a guaranteed value.
The above directions combine industry uses of low-P coatings with this product's 75℃ process features; specific substrates and workpieces must be evaluated by trial plating.
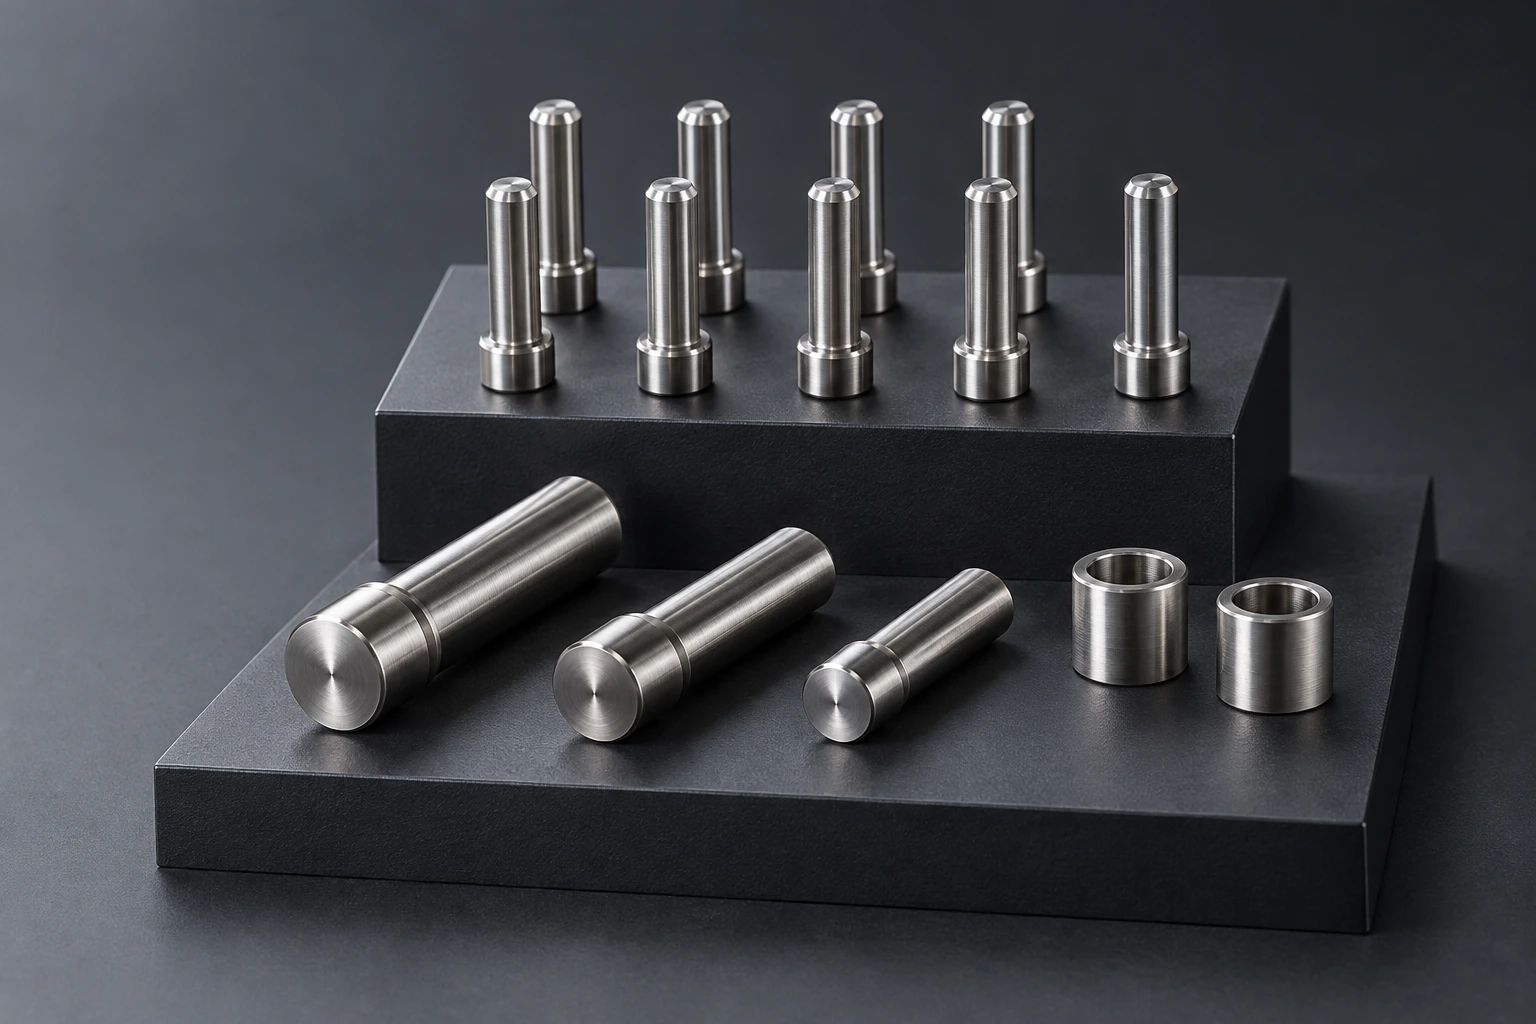
02 / 0.5%–1% coating phosphorus, for lower-P process needs.
Ultra-low-P
Lead-free electroless nickel bath
This is a lead-free ultra-low-P electroless nickel bath with 0.5%–1% coating phosphorus and HV 700 hardness after plating, combining wear resistance, low volume resistivity and magnetic coating characteristics. Application evaluation can focus on low-P requirements for parts such as precision connectors and moving mating parts, with continuous production managed by automatic analysis and replenishment.
Focus on ultra-low-P coatings
Coating phosphorus content of 0.5%–1%, a dedicated version for lower phosphorus requirements.
HV 700 hardness after plating
Combining wear resistance, low volume resistivity and magnetic characteristics to meet functional surface treatment needs.
Supports continuous production
Compatible with automatic analysis and replenishment, easing bath management per this version's process conditions.
Process parameters
- Coating phosphorus content
- 0.5%–1%Interim instructions p.3
- Operating temperature
- 88–94℃Per the manual's operating conditions table
- pH
- 6.00±0.10
- Nickel plating rate
- 10±2 μm/hFresh bath, 90℃
- Nickel sulfate concentration
- 20.0±1.0 g/Las NiSO₄·6H₂O
- Bath load ratio V/A
- 8–20bath volume mL / workpiece surface area cm²
- Coating hardness
- HV 700after electroless plating
Application directions & confirmation conditions
An option for lower phosphorus requirements; below are application directions suitable for verification.
Precision electronic connections
Connectors · terminals · electrical contact structures
Where lower coating phosphorus is explicitly required, this product can be evaluated together with low-resistance needs; contact resistance, soldering and assembly performance must be verified.
Refers to industry uses of low-P coatings; does not mean the ultra-low-P version has completed the same verification.
High-hardness moving mating parts
Valve parts · precision transmission components
For parts with requirements on both composition and as-plated hardness, coating options for wear and mating surfaces can be evaluated around the HV 700 hardness after plating.
Confirm suitability by actual load, friction pair and thickness.
New-energy electrical connections
Busbars · battery connectors
Low-P electroless nickel already has industry uses of this kind. If a design specifies 0.5%–1% phosphorus content, this product can be included in process verification.
Electrical connection, thermal cycling and service environment requirements must be verified.
Hardness uses the latest confirmed value of HV 700; other operating conditions refer to the August 2025 rev.0 technical manual.
Application directions refer to industry data on low-P coatings; suitability of the 0.5%–1% ultra-low-P version must be verified on the specific workpiece.
NI-P / Extremely-low-P continuous production
Coating composition & management features
- Coating system
- Nickel-phosphorus (Ni-P)
- Coating phosphorus content
- Below 1%Phosphorus content remains essentially stable as turnovers increase
- Chemical features
- Lead-free
- Production management
- Automatic analysis · automatic replenishment
03 / Continuous operation, maintaining an extremely-low-P coating.
Extremely-low-P continuous type
Lead-free electroless nickel bath
The extremely-low-P continuous type can continuously form Ni-P coatings with phosphorus below 1%, and coating phosphorus remains essentially stable as turnovers increase. Its lead-free system suits automatic analysis and replenishment, easing bath management in continuous production. Operating temperature is 83–87℃; at make-up at 85℃, the plating rate is 11±2 μm/h.
Extremely low P maintained continuously
The instructions state that coating phosphorus remains essentially stable below 1% as turnovers increase.
Lead-free bath system
Forms extremely-low-P Ni-P coatings with a lead-free electroless nickel bath, suited to process management for continuous production.
Automatic analysis & replenishment
Suitable for automatic analysis and replenishment, helping maintain stable quality in continuous operation.
Process parameters
- Coating phosphorus content
- Below 1%continuous operation; extremely-low-P continuous type instructions p.1
- Operating temperature
- 83–87℃Raise temperature as turnovers increase to manage plating rate
- pH
- 6.00±0.10
- Nickel plating rate
- 11±2 μm/hat make-up, 85℃
- Nickel sulfate concentration
- 20.0±2.0 g/Las NiSO₄·6H₂O
- Bath load ratio V/A
- 8–12bath volume mL / workpiece surface area cm²
Selection focus & production conditions
Confirm the process per the extremely-low-P continuous type instructions, around the extremely-low-P coating target and continuous production conditions.
Extremely-low-P composition requirement
Ni-P · phosphorus below 1%
For process evaluation aiming to continuously obtain extremely-low-P Ni-P coatings; the instructions explicitly stress phosphorus stability as turnovers increase.
Continuous operation & rate management
83–87℃ · automatic analysis & replenishment
The reference condition for plating rate is 85℃ at make-up. The instructions require raising temperature within the operating range as turnovers increase to manage the nickel plating rate.
Other functional or substrate needs
For thin-film resistor uses, see thin-film resistor functional coating; for glass, ceramics and similar substrates, see neutral low-temperature electroless nickel for glass & ceramics.
Parameters are based on pp.1 and 3 (PDF pp.3 and 5) of the "Extremely-low-P continuous type instructions" (2023.05). Phosphorus content keeps the original wording "below 1%"; the rate is data at make-up at 85℃.
Coating hardness and specific workpiece performance must be confirmed separately according to the actual process of the extremely-low-P continuous type.
02 / Selecting for wear resistance and precision fit
Low-P option
Coating phosphorus content is 1%–3% and operating temperature 85–90℃. Process evaluation centers on as-plated hardness, wear resistance and the fit requirements of specific parts.
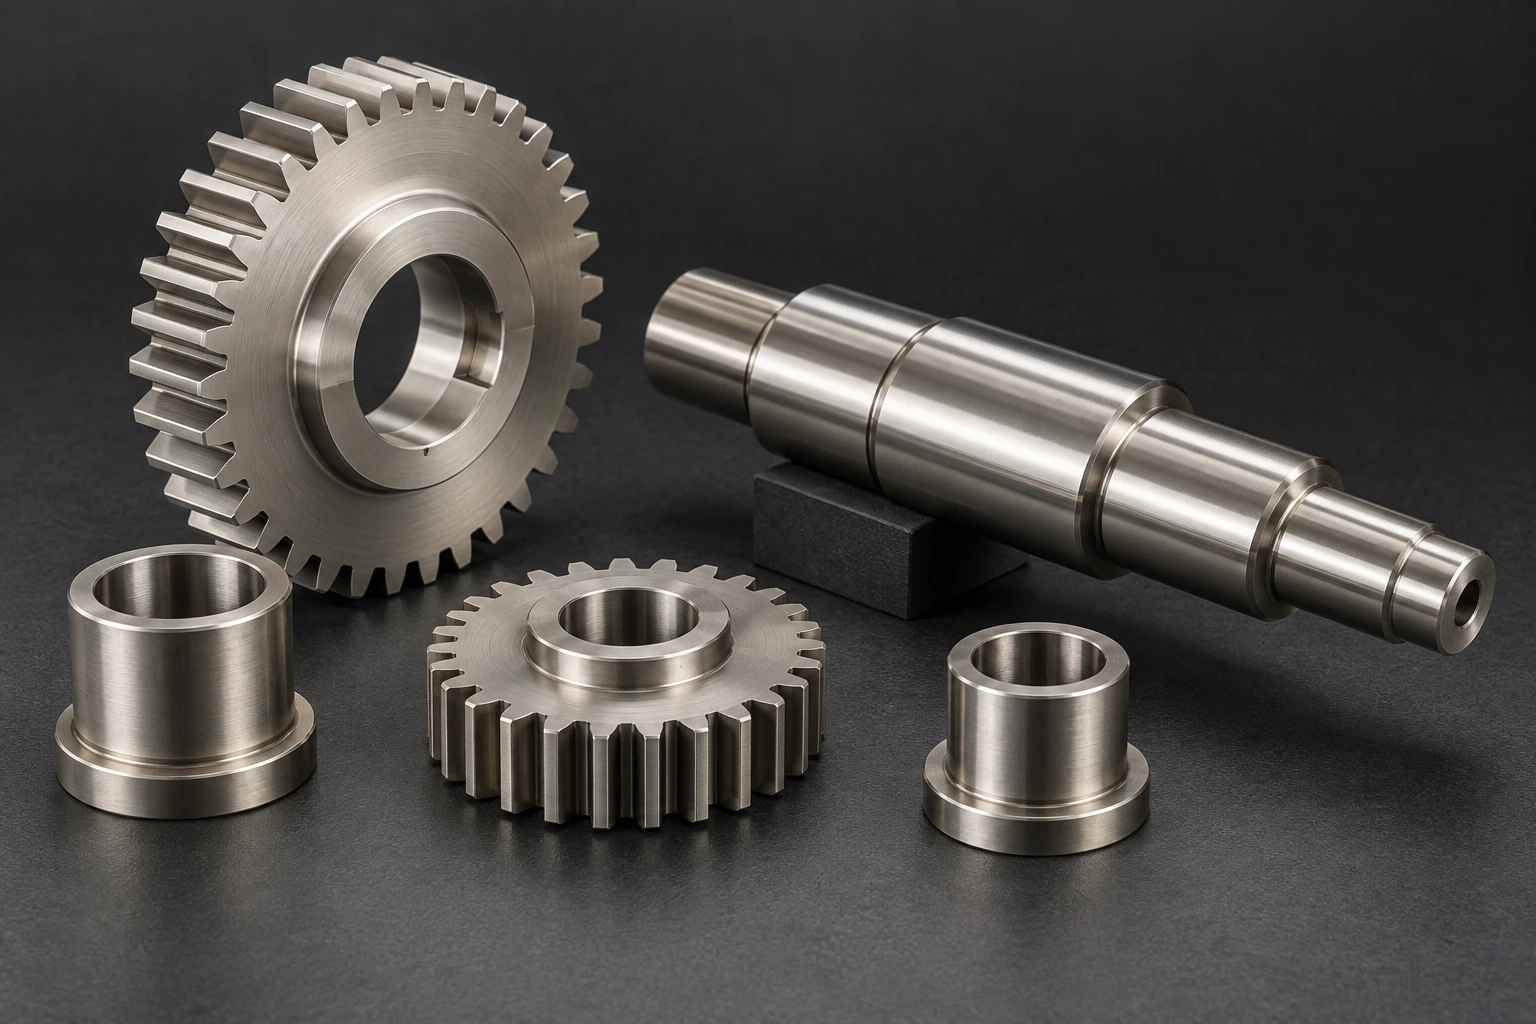
04 / 1%–3% low-P coating, chosen for wear resistance and precision fit.
Low-P
Lead-free electroless nickel bath
This is a lead-free low-P electroless nickel bath with 1%–3% coating phosphorus and HV 650 hardness after plating, combining wear resistance, low volume resistivity and magnetic characteristics. It can be selected for applications such as mold tooling, valves, transmission components and hydraulic/pneumatic parts. Operating temperature is 85–90℃; it supports automatic analysis and replenishment for easy bath management in continuous production.
Supports production takt
At make-up at 87℃, the manual indicates a nickel plating rate of 17±2 μm/h.
HV 650 hardness after plating
Combined with wear resistance and low volume resistivity, a low-P coating option for functional parts.
Continuous bath management
Supports automatic analysis and replenishment, helping maintain bath conditions and stable quality.
Process parameters
- Coating phosphorus content
- 1%–3%coating phosphorus content
- Operating temperature
- 85–90℃manual operating conditions
- pH
- 6.40±0.10
- Nickel plating rate
- 17±2 μm/hfresh bath, 87℃
- Nickel sulfate concentration
- 24.0±2.0 g/Las NiSO₄·6H₂O
- Bath load ratio V/A
- 8–20bath volume mL / workpiece surface area cm²
- Coating hardness
- HV 650after electroless plating
Application directions & confirmation conditions
Learn the typical application directions of low-P coatings around specific parts and functional needs.
Molds & forming tooling
Molds · plungers · tooling
For areas subject to repeated forming and contact wear, selection focuses on as-plated hardness and wear resistance. Public industry data lists related uses of low-P coatings.
The solution should be confirmed with workpiece shape, thickness and surface precision.
Valves & motion mechanisms
Valve parts · gearbox components · hydraulic/pneumatic parts
For surfaces with frequent motion and precision fit, the hardness and wear performance of low-P coatings can be evaluated while controlling coating thickness.
Confirm by trial plating against load, media and fit tolerances.
Electronic & electrical connections
Connectors · terminals · busbars · battery connectors
For low-resistance and assembly needs of electrical connection parts, a low-P nickel layer and suitable thickness can be selected together with the substrate and subsequent connection method.
Solderability and connection reliability must be confirmed in the actual structure.
Application scenarios refer to low-P electroless nickel industry data; specific thickness, fit dimensions and service conditions must be confirmed with the workpiece.
Ni-P part application data
Starting from actual parts, learn about Ni-P electroless nickel applications in automotive and precision machinery.
The following Ni-P electroless nickel case images help explain part application needs and do not correspond directly to the four chemicals on this page. Specific selection must be confirmed with the substrate, target performance and process conditions.
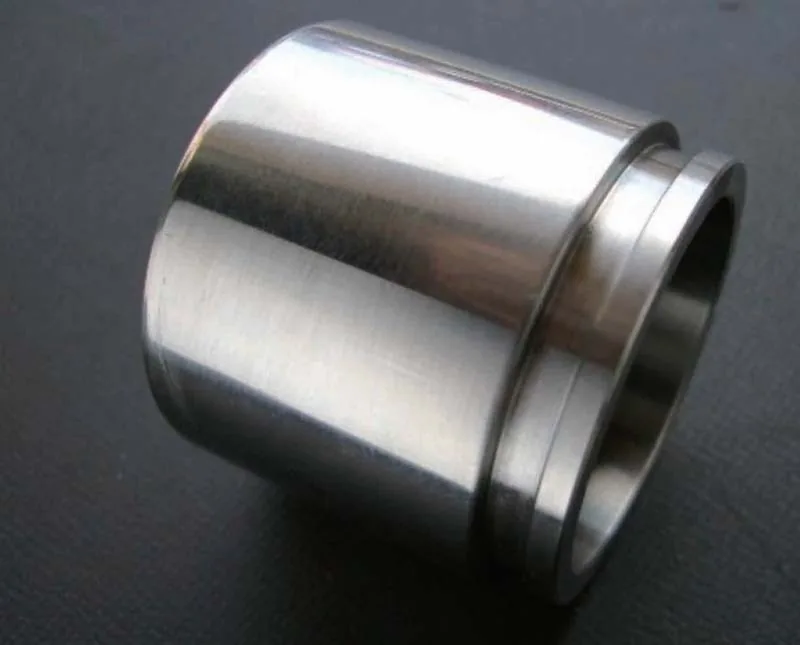
Automotive braking
Brake piston
Used in brake devices; the surface treatment focuses on wear resistance.
See application conditions ↗
Automotive transmission
Clutch hub
Used in manual transmission mechanisms, balancing sliding properties and wear resistance.
See application conditions ↗
Automotive braking
Brake wheel cylinder
Used in brake devices, focusing on wear resistance of moving parts.
See application conditions ↗
Fuel injection control
Roller bracket
Used in engine fuel injection control devices, focusing on wear resistance, rust prevention and dimensional accuracy.
See application conditions ↗Technical data & application reference notes
Phosphorus content listed refers to coating phosphorus content. Parameters are compiled from product manuals and the latest confirmed information; actual performance depends on substrate, pretreatment, coating thickness and bath management.
Product parameters are compiled from the corresponding instructions and confirmed values; industry applications are selection directions and do not mean this series has been verified on all listed workpieces. Corresponding process data can be requested at the end of the page.
Data for the extremely-low-P continuous type is based on the "Extremely-low-P continuous type instructions" (2023.05): PDF p.3 (text p.1) lists the extremely-low-P, lead-free and automatic analysis/replenishment features, and PDF p.5 (text p.3) lists the operating conditions. Each product's parameters are listed separately for its process.
Confirm a low-P electroless nickel solution with an engineer
For chemical selection, please provide the substrate, target performance and line conditions; for parts plating, also specify quantity and drawing requirements.