SPECIALTY ELECTROLESS ALLOY
Ni-P-Co-WNi–P–Co–W
Lubricious sliding and wear resistance,
with high hardness as plated.
A quaternary electroless system of nickel, phosphorus, cobalt and tungsten. Combining high as-plated hardness, wear resistance and sliding properties, for lubricated conditions in bushings, transmission parts and hydraulic sliding areas.
High as-plated hardnessWear resistance · lubricated sliding
≥650 HV
Material instructionsSliding properties
Functional features listed in the material instructionsWear performance
Evaluated with the counterpart, load and lubrication conditions01 / MATERIAL ADVANTAGES
Hardness, lubricated sliding and wear resistance.
Evaluate the suitability of Ni-P-Co-W coatings
around the part's actual friction, sliding and production conditions.
High hardness as plated
Without heat treatment, the instructions list a coating hardness of 650 HV or above. For parts where heat treatment is restricted, evaluate with substrate and dimensional requirements.
AS-PLATED HARDNESSLubrication & sliding properties
The instructions explicitly list sliding properties. For contact surfaces such as bushings and transmission parts, evaluate friction at start-up and during sustained sliding with the friction pair, speed and lubrication state.
LUBRICITY & SLIDINGWear-resistant contact surfaces
The instructions list wear resistance as a main feature. For mechanical parts with repeated contact, confirm wear inspection, coating thickness and post-plating fit dimensions together.
WEAR RESISTANCESuited to continuous production management
Supports automatic analysis and replenishment for controlling bath condition during production. Establish an appropriate process window with production takt and workpiece requirements.
PROCESS CONSISTENCY02 / LUBRICITY & SLIDING
Lubrication & sliding:
look at contact behavior on its own.
The material instructions list excellent wear resistance and sliding properties as main features. For bushings, transmission parts and hydraulic sliding areas, evaluate contact friction, motion resistance and wear under actual lubrication conditions.
Material instructions (2023.5), text p.1: qualitative description of wear resistance and sliding properties.
Confirm sliding behavior with these conditions
- Friction pair & contact mode
- Counterpart material, contact surface geometry, reciprocating or rotary motion.
- Load & motion speed
- Focus on friction at start-up and during sustained motion, and check actual load and speed.
- Lubrication & surface condition
- Lubricant, oil supply conditions, coating thickness and roughness of mating surfaces.
Existing data does not list friction coefficients or friction reduction for the same material; related metrics are confirmed by comparison under agreed conditions and samples.
03 / SELECTED TECHNICAL DATA
Key parameters, clearly presented.
Based on the corresponding material's technical data.
Read values together with conditions for better-grounded selection.
Ni–P–Co–W
Quaternary alloy
electroless system
An alloy system of nickel, phosphorus, cobalt and tungsten yields a coating suited to functional surface treatment.
As-plated hardness and heat-treated hardness should be understood separately. Heat treatment temperature is also not the same as the part's long-term service temperature.
| Item | Reference value | Conditions / notes |
|---|---|---|
| Alloy system | Ni–P–Co–W | Nickel, phosphorus, cobalt, tungsten |
| As-plated hardness | ≥650 HV | Without heat treatment |
| Lubrication & sliding | Qualitative sliding properties | Specific friction behavior is verified by counterpart, load, speed and lubrication state |
| Wear resistance | Qualitative wear resistance | Listed as a main feature in the material instructions; wear behavior is evaluated per operating conditions |
| Deposition rate | 19 ± 2 μm/h | Fresh bath, 88℃ |
| Operating temperature | 88–94℃ | Adjust with bath age to manage deposition rate |
| Operating pH | 6.00 ± 0.10 | Instruction operating conditions |
Source: Ni-P-Co-W Chinese instructions (2023.5), text pp.1 and 3. Thickness, pretreatment and acceptance criteria for actual workpieces must be confirmed with the application.
04 / HARDNESS & HEAT TREATMENT
See the hardness, and see the test conditions.
The original technical data records how hardness changes
over the bath's service cycle under different heat treatment conditions.
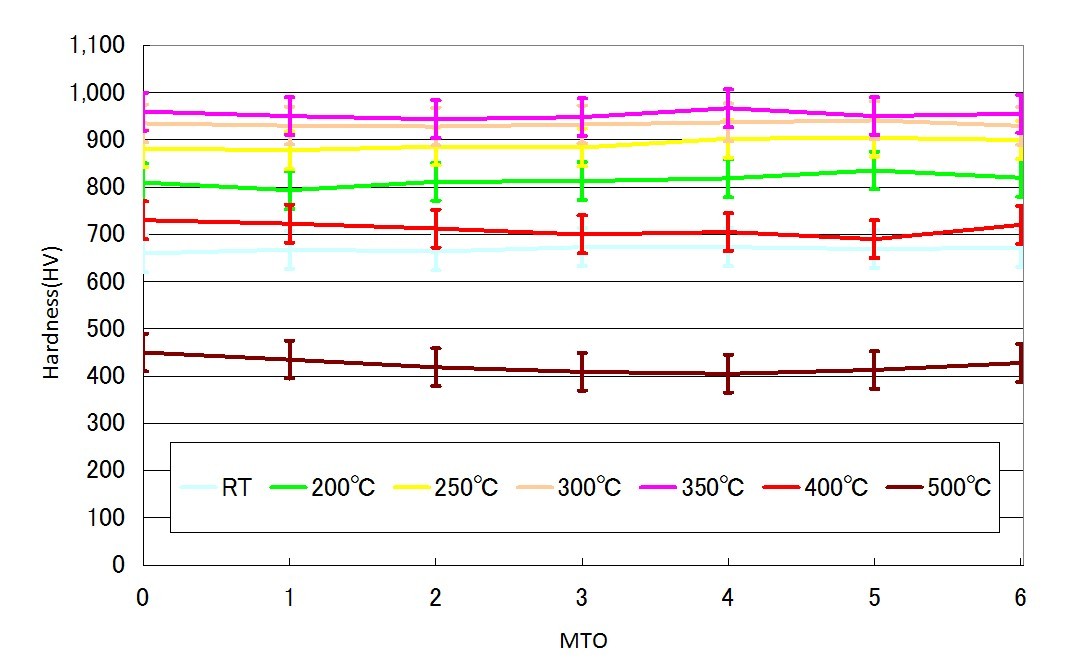
After 350℃ × 1 h heat treatment
approx. 950 HV
This group of curves lies at about 950 HV. This is an approximate reading from the original chart, reflecting results for the specified specimens and test conditions.
- Specimen substrate
- SPCC
- Coating thickness
- 30 μm
- Test load
- 100 g
- Measurement method
- Vickers microhardness
In the chart, RT means not heat-treated; MTO is the bath metal turnover. Temperatures of other curves are heat treatment temperatures, each held for 1 hour.
See data sources & parameter notes
Instructions: Ni-P-Co-W electroless plating instructions, May 2023 edition. As-plated hardness and product features on text p.1; deposition rate, temperature and pH on text p.3.
Test data: Ni-P-Co-W electroless plating English technical data, June 2020. Hardness chart and test conditions on p.4.
Hardness testing shows material performance under specified conditions; it does not directly represent a part's wear life or long-term temperature resistance. Specific workpieces are subject to agreed processes and sample verification results.
05 / APPLICATION DIRECTIONS
Start from operating conditions
to match the functional surface.
For mechanical parts with wear, lubrication and sliding needs,
Ni-P-Co-W can be included in process selection and sample evaluation.
Bearing & bushing parts
Focus on start-up resistance and friction and wear in sustained sliding, and check post-plating fit dimensions.
Gears & transmission parts
Check rotation speed, load and lubricating oil conditions, and evaluate contact surface friction and wear.
Hydraulic pistons & sliding parts
Check reciprocating speed, media and seal counterparts, and evaluate sliding resistance and surface wear.
The above are application evaluation directions; specific substrates, structures and service conditions must be confirmed by technical staff.
LET’S TALK ABOUT YOUR PART
Bring selection down to your workpiece.
Provide the substrate, target thickness, operating temperature and friction conditions to discuss a Ni-P-Co-W application plan.